Best Profile Projector Machine for Precision Dimensional Inspection
2026-09-27
When every micron counts, a standard profile projector just won't cut it. In precision dimensional inspection, the right optical comparator can mean the difference between a pass and a costly recall. In this guide, we break down what actually matters when choosing the best profile projector machine—and why teams that demand repeatable accuracy are turning to JATEN.
Why a Crisp Projected Image Depends on More Than Just Magnification
It’s tempting to think that cranking up the magnification is all it takes to get a sharp projected image, but that assumption falls apart quickly when you look at the actual optical chain. Magnification only determines how large the picture appears; it says nothing about how well fine details survive the journey from lens to screen. A projector with a high zoom ratio but a mediocre lens will still smear edges, introduce color fringing, or lose micro-contrast in dense textures. The real measure of clarity is the optical system’s modulation transfer function, which describes how faithfully contrast is preserved at different spatial frequencies. If that function drops off early, no amount of magnification will bring back the lost information.
Another factor that often gets overlooked is the projector’s native contrast and the uniformity of its light source. You can have a high-resolution imaging chip, but if the black levels are elevated or the illumination falls off toward the corners, the image will look flat and hazy regardless of pixel count. Human perception of sharpness is tightly linked to local contrast—the crisp transition between a bright edge and a dark background. When stray light bounces around inside the optics or the lens has poor baffling, those transitions get polluted, and the picture loses its snap. This is why two projectors with identical resolution specs can look completely different in a side-by-side comparison.
Finally, the projection surface itself plays a decisive role that no amount of optical zoom can fix. A smooth, matte screen with controlled gain preserves the fine structure of the image, while a textured wall or a glossy board scatters light unpredictably, creating a subtle blur or hotspotting. Even the color of the surface matters—warm off-white walls shift the white balance and reduce perceived sharpness. Achieving a truly crisp projected image demands attention to the entire pipeline: the lens quality, the light engine’s uniformity, the processing electronics, and the screen characteristics. Magnification is just one dial among many, and often not the most important one.
Choosing the Right Lens and Screen Size for Your Tolerance Band
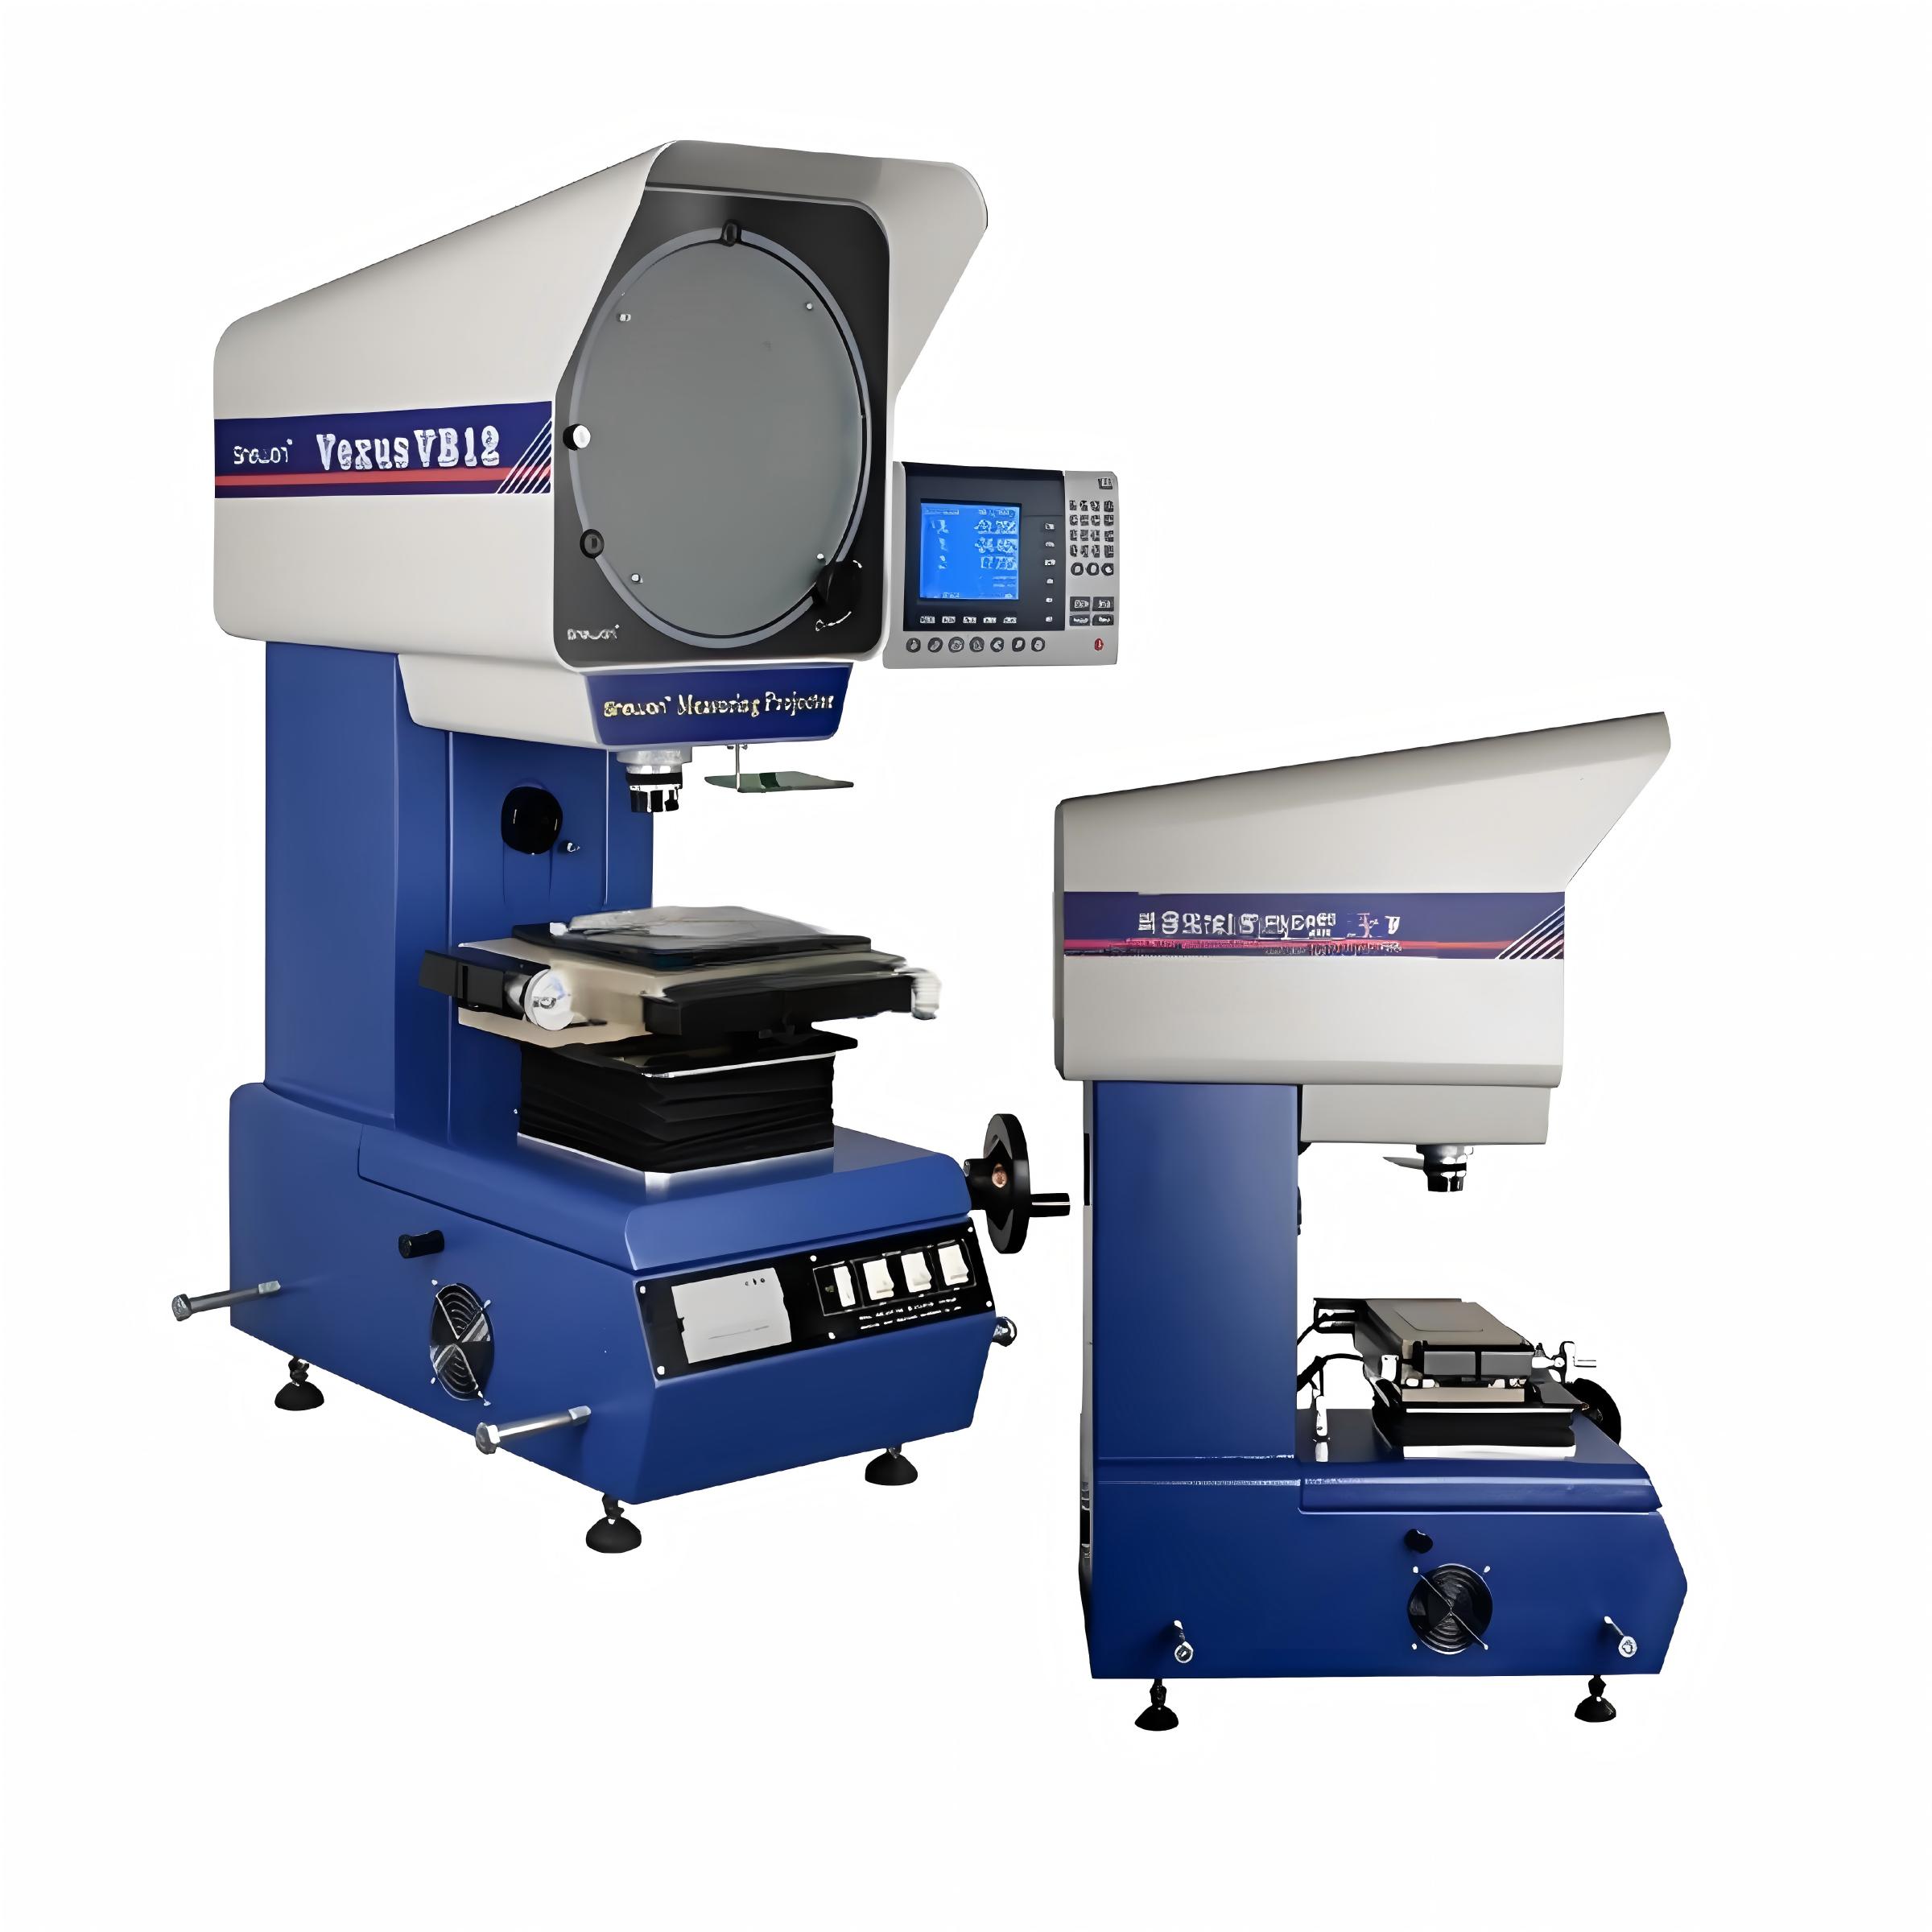
Matching a lens to your tolerance band starts with one practical question: how much of the part do you actually need to see at once? If the feature spans only a few millimeters and the permissible variation is tight, a higher magnification lens makes sense because it spreads those small deviations across more of the sensor or screen. But that narrows the field of view, so you may end up repositioning the part for every measurement. The opposite problem shows up with wide field lenses—you capture the whole region, but fine deviations get compressed into just a pixel or two and become easy to miss.
Screen size plays a supporting role, not a corrective one. A larger display can make small features easier for an operator to read, but it does not add measurement resolution. If the lens and camera cannot resolve a tenth of your tolerance band, enlarging the image on a bigger monitor simply makes the uncertainty larger and more obvious. What matters is that the screen diagonal, viewing distance, and magnification together keep the minimum tolerance increment visually separable without forcing the operator to squint. Better to have a slightly smaller screen with clean, well-scaled pixels than a large one that stretches a marginal image.
A useful starting point is to divide the tightest tolerance by ten and treat that as your required resolvable increment. Then work backward: define the largest field of view you must inspect in one setup, divide that by the available sensor or screen resolution, and see if the resulting pixel size is smaller than your required increment. If not, you either increase magnification, reduce the field of view, or step up to a higher resolution system. Screen size then becomes a matter of operator comfort—choose one that lets you read the scaled image without leaning in, while keeping the lens and sensor doing the real measurement work.
Vertical vs. Horizontal Light Paths: Matching Design to Part Geometry
Choosing between a vertical and a horizontal light path often starts with the part's silhouette. Tall, upright components—such as connectors, pins, or stacked assemblies—tend to suit a vertical path, where illumination and imaging move along the same axis as the part's height. This keeps top surfaces and recessed features evenly lit without fighting the geometry.
Flat, wide, or elongated parts, by contrast, often benefit from a horizontal setup. A horizontal light path can sweep across the longest dimension, reducing shadowing on low-profile edges and making it easier to capture side-wall defects. It is not a rigid rule, but matching the optical axis to the part's dominant plane usually improves contrast and repeatability.
When a part mixes both tall and flat regions, a tilted or switchable path may be the practical compromise. The goal is to align the light direction with the geometry you need to inspect most critically, rather than forcing a standard configuration onto an awkward shape.
Edge Detection Algorithms That Reduce Operator-to-Operator Variability
Manual tracing of anatomical structures in medical images often suffers from noticeable differences between operators, even when they follow the same protocol. Edge detection algorithms address this by replacing hand-drawn boundaries with mathematically defined transitions between tissue types. Rather than relying on individual judgment about where a boundary sits, these methods use intensity gradients, texture shifts, or model-based energy minimization to locate edges consistently. The result is a reproducible contour that does not drift with fatigue, training background, or personal interpretation.
A key advantage of automated edge detection is its ability to apply the same criteria across every image and every session. For example, gradient-based detectors like Canny or Laplacian of Gaussian identify edges at local maxima of intensity change, while active contour models refine an initial guess by balancing internal smoothness with external image forces. Because these computations are deterministic, the output depends on the algorithm parameters—which can be fixed and audited—rather than on the operator's hand steadiness or visual acuity. In multi-center studies, this reduces the need for extensive inter-rater reliability testing and enables tighter quality control.
Implementing such algorithms does not eliminate all variability, since choices like pre-processing filters, threshold values, and initialization still require some setup. But once those are standardized, the remaining variation is typically far smaller than what arises from manual delineation. Many clinical research teams adopt edge detection not only for speed but also to ensure that repeated measurements of the same structure yield nearly identical results across different technicians. This consistency directly supports longitudinal studies, machine learning training data creation, and any application where small boundary differences could change diagnostic or quantitative outcomes.
Calibration and Stage Alignment: Keeping Your Readings Honest
A stage that drifts even a few microns will quietly distort every measurement you take. Calibration is not a one-time checkbox; it's a habit that keeps your data tied to physical reality. Without it, you're not observing a sample—you're observing a machine's mood.
Start by zeroing the stage against a known reference grid or micrometer standard. Move through the full travel range at low speed and watch for backlash, tilt, or non-orthogonality between the X and Y axes. If the stage does not return to the same coordinates after a full cycle, your alignment is off, and so is everything downstream.
Keep a simple logbook of when you calibrated, what standards you used, and any corrections applied. That record matters more than the brand of your equipment. Readings stay honest only when the platform beneath them is repeatedly questioned and verified.
From Shadowgraph to Digital Comparator: What Modern Upgrades Actually Improve
For decades, a shadowgraph's usefulness depended almost entirely on an operator's ability to judge where a fuzzy, magnified silhouette matched a printed overlay. That visual guesswork introduced subtle but costly errors, particularly on low-contrast edges or parts with repeating geometries. A digital comparator replaces the eyeball with a camera and sub-pixel edge detection, so the first genuine improvement is not higher magnification but repeatability. The same feature measured twice yields the same number, regardless of who is at the machine.
The second practical upgrade is speed through automation. Instead of manually repositioning a part and comparing it against a full chart each time, a modern system lets you store part programs, recall a setup in seconds, and run a one-click measurement routine. Live on-screen imaging with adjustable LED illumination also reveals details that were easy to miss on a traditional glass screen, while direct CAD overlay removes the need to maintain physical transparencies for every part number.
Data handling marks a third shift. Results flow into SPC or inspection reports without handwritten notes, cutting transcription errors and making traceability automatic. That may sound mundane, but in a production environment it often saves more time than the measurement itself. Not every digital feature matters equally, though; the upgrades that truly pay for themselves are reliable edge detection, faster part changeovers, and clean data output, not just a higher-resolution display.
FAQ
A solid machine earns its keep through edge clarity, stage stability, and repeatable magnification. Look for telecentric optics that keep contours sharp even near the screen edges, a rigid stage with minimal backlash, and a lens set that actually matches your part size. Cheap projectors often struggle with distortion at high magnification or drift after repeated stage movement.
Vertical machines work well for flat parts, stamps, and small turned components because you simply lay the part on the glass. Horizontal projectors suit heavier or awkwardly shaped workpieces, especially long shafts or parts that need to be held in a fixture. If your parts are mostly round and bulky, horizontal is usually the better call; for thin, flat items, vertical saves time.
Yes, angle and radius measurements are standard. Use the rotating screen and vernier scale for angles, and overlay radius charts or digital arc templates for radii. The catch is that screen-based radius charts are only as good as your alignment and magnification calibration. For critical radii, a digital readout with edge detection reduces operator bias.
Transmitted light works for silhouettes, but a low-angle reflected light attachment often brings out recesses, shoulders, and surface steps. Avoid flooding the part with excessive light; too much brightness washes out thin edges. A green filter can also improve contrast for polished metal parts by reducing glare.
Screen size matters mainly for viewing multiple features at once. A 300 mm screen is fine for most small parts, but if you inspect long threads, gears, or stamped patterns, a 400–500 mm screen lets you see the full profile without repositioning. However, bigger screens alone don't improve accuracy; optical quality and stage precision matter more.
Keep the stage and glass clean with lint-free wipes, and never use compressed air near lens surfaces because it can force dust deeper. Lubricate the leadscrews sparingly with the recommended grease, and check calibration monthly with a traceable glass scale. If the image gets hazy, check the collimator lens and mirror alignment before assuming the bulb is weak.
They help when you need documented results or want to reduce eye fatigue during repetitive checks. A good camera with edge-detection software can improve repeatability on fuzzy edges, but it won't fix poor optics or stage play. If your shop does mostly quick pass/fail checks, a plain screen works fine; for formal reports, digital is worth the cost.
Many operators forget to refocus after changing magnification or stage height. A sharp image on the screen doesn't guarantee the part is at the correct focal plane for measurement. Always verify focus with the crosshair or a known feature, and avoid measuring edges near the screen border where distortion is often highest.
Conclusion
A profile projector that earns its place on the quality bench does far more than offer a high magnification number. The crispness of the projected image is shaped by the illumination system, condenser lens alignment, and the overall optical correction, not just the objective's power. When the tolerance band is tight, matching the lens magnification and screen diameter to the feature size prevents both misleading edge thickness and needless re-fixturing. A 10x lens on a 300 mm screen may be ideal for a small turned profile, while a 20x lens might enlarge the image beyond the screen's usable center and introduce distortion at the periphery. The light path orientation matters too: horizontal projectors naturally hold cylindrical shafts between centers, whereas vertical systems simplify the staging of flat stampings, gears, and plastic moldings. Choosing the wrong path can force awkward clamping, which itself becomes a source of measurement scatter.
Beyond optics, the best modern machines rely on edge detection algorithms that sample the transition from bright to dark in a repeatable way, minimizing operator-to-operator differences in deciding where a shadow begins. These tools are only as trustworthy as the stage alignment and calibration routine behind them. Regular checks with a certified glass scale, attention to backlash, and temperature stability keep readings honest over months of use. The shift from pure shadowgraph to digital comparator is not merely cosmetic: camera-based capture, motorized stages, and automated pass/fail routines cut inspection time and record data without transcription errors. Yet the core requirement remains a rigid, well-aligned optical train. You are not paying for pixels alone; you are paying for an instrument that will not drift, distort, or soften the edge you're trying to measure.
Contact Us
Contact Person: Volien
Email: [email protected]
Tel/WhatsApp: +86 18029161762
Website: https://www.jatentech.com/